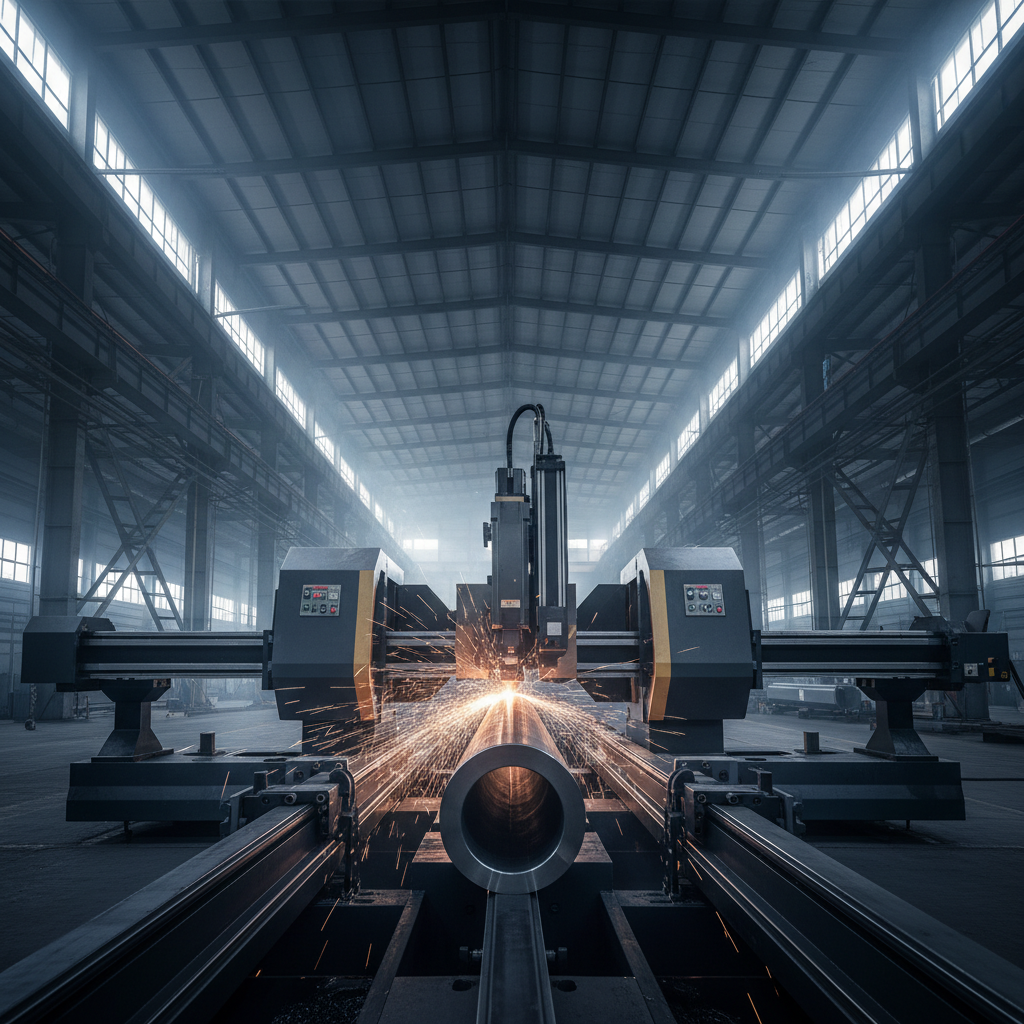
The global industrial landscape relies heavily on the efficient production of high-quality steel tubing, where precision and durability are paramount. At the heart of this production process is advanced welded pipe equipment, which transforms flat strip steel into structural conduits capable of withstanding immense pressure and environmental stress. By integrating mechanical forming and thermal welding, these systems ensure that infrastructure from urban skyscrapers to energy pipelines remains secure and sustainable.
Modern manufacturing challenges demand a shift toward higher automation and tighter tolerances to reduce material waste and operational costs. Traditional piping methods often struggle with consistency in wall thickness and longitudinal seam integrity, leading to potential failure points in critical applications. This necessitates the adoption of sophisticated machinery that can handle varying grades of steel while maintaining high-speed output without compromising the structural characteristics of the final product.
Investing in high-performance welded pipe equipment allows manufacturers to optimize their production lines for specific diameters and wall thicknesses, ensuring compliance with international ISO and ASTM standards. By understanding the synergy between uncoiling, forming, welding, and sizing, companies can achieve a competitive edge in the global metalworking market, delivering products that offer superior reliability and long-term value.
Technical Foundations of Welded Pipe Equipment
The fundamental operation of welded pipe equipment involves the precise transformation of strip steel into a cylindrical form. For a system handling strip widths between 238-279mm and thicknesses from 2.0 to 5.0mm, the process begins with high-grade materials such as Q195-Q345 steel. This ensures that the resulting pipes, typically ranging from φ76 to φ89mm in diameter, possess the requisite tensile strength and ductility for industrial use.
Achieving a forming speed of 60-80m/min requires a delicate balance between torque and precision. The mechanical design must prevent material buckling while ensuring the longitudinal seam is perfectly aligned for welding. By utilizing calibrated rollers and high-performance drive systems, the equipment minimizes length accuracy deviations to within 0-6 mm, ensuring that every segment produced meets strict commercial tolerances.
The Critical Role of Auxiliary Machinery
A production line is only as strong as its weakest link, which is why auxiliary components are vital. The process starts with a single-station manual uncoiler capable of adapting to inner diameters of Ф762mm and outer diameters of Ф1800mm. This unit supports coils up to 5 tons, providing a steady feed of raw strip steel into the system, which is essential for preventing abrupt tension changes that could warp the material.
Following the uncoiler, the shearing and welding station employs hydraulic cutting and pneumatic pressing platforms to prepare the strip. While manual welding is utilized to join the ends of the strip, the precision of the pneumatic press ensures that the joint is flush. This preparation phase is critical because any misalignment here will be magnified during the forming process, potentially leading to defective pipe seams.
To maintain continuous production, a four-roller delivery machine and a cage looper are integrated. The delivery machine, powered by an 18.5KW motor, feeds material at speeds up to 140m/min, while the cage looper acts as a buffer. This storage mechanism allows the forming and sizing machines to operate without interruption even if the uncoiler requires adjustment, maximizing the overall OEE (Overall Equipment Effectiveness) of the welded pipe equipment.
Main Machine Composition and Precision Forming
The core of the welded pipe equipment is the main forming mill, which utilizes a complex arrangement of rollers to shape the steel. The sequence includes passive seven-roller leveling and feeding vertical rollers, followed by a rigorous forming stage consisting of 7 flat and 8 vertical rollers. This phased approach ensures the strip is gradually curved without inducing internal stresses that could lead to premature cracking.
Sizing is the next critical phase, employing 6 flat and 6 vertical rollers to lock in the final diameter of φ76-φ89mm. The machinery is powered by a massive 250KW DC motor and a ZLY280-10 reducer, providing the immense torque necessary to deform 5.0mm thick steel. The use of 40Cr material for horizontal and vertical shafts, which are quenched and tempered, ensures that the rollers maintain their geometry under extreme pressure.
The final stages of the main machine include extrusion, scraping, and a cooling water tank to stabilize the temperature of the welded seam. A specialized "Turkish ear head" with 8 rollers provides final shaping and alignment. The entire transmission is handled by a ZG35# gear box featuring spiral bevel gears with a module of m=12, ensuring smooth power delivery and minimal vibration throughout the welded pipe equipment operations.
Efficiency Metrics in Pipe Production
Measuring the productivity of welded pipe equipment requires looking at the intersection of speed and accuracy. With forming speeds reaching 80m/min and a computer-controlled flying saw capable of 15 cuts per minute, the throughput is significantly higher than manual or semi-automated lines. The synchronization between the drive motor and the sawing trolley is what allows for the ±3 mm length accuracy.
The integration of DC drive systems for the main mill and the flying saw provides the necessary control over acceleration and deceleration, which is vital for maintaining the wall thickness of 2-5 mm. By analyzing the power consumption of the 250KW main motor against the output volume, operators can optimize the feed rate to ensure maximum efficiency without overstressing the mechanical components.
Performance Ratings of Welded Pipe Equipment Configurations
Precision Cutting with Computer Flying Saws
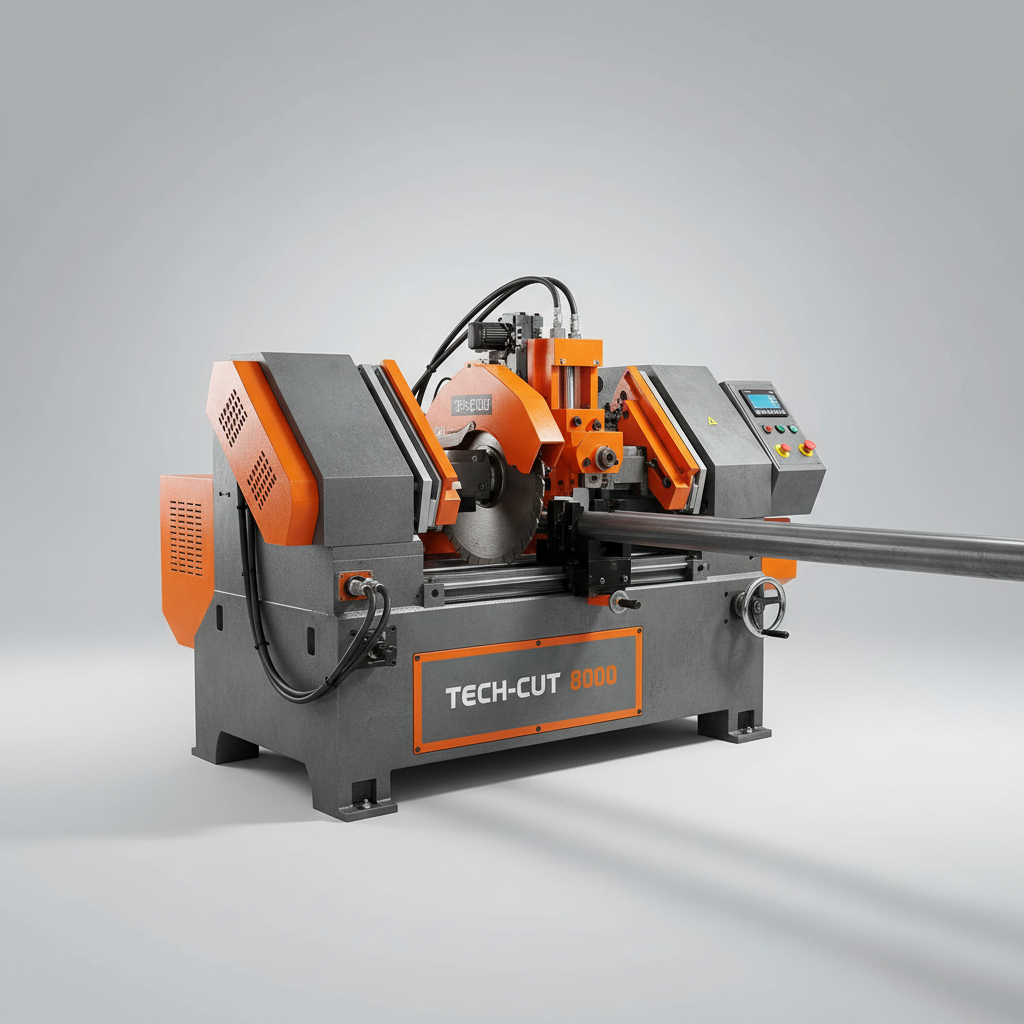
The computer flying saw machine is a marvel of synchronization within the welded pipe equipment ecosystem. It consists of a precision bed, gear rack boxes, and a high-speed saw car that matches the speed of the moving pipe. By using a speed measurement system and a drive motor (22KW DC), the saw car accelerates to 80m/min, allowing the Ф900mm saw blade to cut the pipe without stopping the production line.
This "flying" action is what enables the machine to achieve a maximum of 15 cuts per minute with a fixed length accuracy of ±3 mm. The air system, operating at 5-7Kg/cm², ensures the fixture holds the pipe securely during the cut, preventing slippage or deformation. This level of automation transforms the end of the line from a bottleneck into a high-efficiency output center.
Stress Relief and Straightening Processes
After the pipe has been formed and welded, it often retains internal stresses that can cause bending or warping. The straightening machine in the welded pipe equipment line is designed specifically to eliminate these defects. Utilizing a four-column frame structure with four upper passive rollers and two lower active rollers, the machine applies controlled pressure to flatten the pipe.
The rollers are crafted from GCr15 material with a hardness of HRC60-65, ensuring they do not wear down when processing hard steel pipes. A manual worm gear is used to press the upper rollers down, allowing the operator to fine-tune the straightening force based on the wall thickness of the pipe (2.0-5.0mm).
With a straightening speed of 100m/min, this process ensures that the final product maintains a perfect linear profile. The specific 30° angle between the straightening roller and the steel pipe is mathematically optimized to distribute pressure evenly, preventing the pipe from becoming oval-shaped while removing the "wave" effect often seen in low-end welded pipe equipment.
Material Specifications and Performance Analysis
The success of any welded pipe equipment setup depends on the compatibility between the machine's mechanical limits and the material properties. Using Q195 and Q345 carbon steels provides a balance of weldability and structural strength. When the strip thickness reaches 5.0mm, the machine's 250KW motor and quenched 40Cr shafts become essential to prevent mechanical deflection.
Furthermore, the choice of GCr15 for the straightening and feeding rollers ensures that the equipment can withstand the abrasive nature of steel over millions of cycles. The use of spiral bevel gears in the gearbox reduces noise and vibration, which is a key indicator of long-term machine health and precision.
Ultimately, the integration of these components allows for a seamless transition from a raw steel coil to a finished, straightened, and precisely cut pipe. The following table summarizes the critical technical thresholds that define the performance of this specific welded pipe equipment configuration.
Technical Specification Summary for Welded Pipe Equipment
| Component |
Material/Spec |
Operational Parameter |
Performance Impact |
| Main Drive Motor |
DC Z4-280-42 |
250KW |
High torque for 5mm strips |
| Forming Shafts |
40Cr (Quenched) |
Ф100mm/Ф60mm |
Prevents shaft deflection |
| Straightening Rollers |
GCr15 |
HRC60-65 |
Extreme wear resistance |
| Flying Saw |
AC 55KW / DC 22KW |
15 cuts/min |
High-speed precision length |
| Gear Box |
ZG35# Spiral Bevel |
Module m=12 |
Smooth power transmission |
| Raw Material |
Q195-Q345 Steel |
2.0-5.0mm Thick |
Structural integrity/weldability |
FAQS
This specific equipment is designed to handle strip steel with a thickness ranging from 2.0mm up to 5.0mm. To achieve this, the machine utilizes a high-torque 250KW DC motor and quenched 40Cr shafts to ensure the material is formed accurately without causing mechanical strain on the rollers.
The flying saw uses a sophisticated speed measurement system and a DC drive motor to match the exact speed of the moving pipe (up to 80m/min). By synchronizing the saw car's travel with the pipe's movement, it achieves a fixed length accuracy of ±3 mm, ensuring minimal waste and consistent product quality.
The cage looper serves as a raw material buffer between the delivery machine and the forming mill. It allows the main forming and sizing machines to maintain continuous production even if the uncoiler needs to be paused or adjusted, preventing costly downtime and ensuring a steady flow of material.
The equipment uses high-grade alloys for its critical components. Forming and extrusion shafts are made from 40Cr steel that is quenched and tempered. Straightening rollers are made from GCr15 bearing steel with a hardness of HRC60-65, which is essential for resisting the abrasive wear of processing carbon steel.
Yes, the system is designed for steel pipe specifications between φ76mm and φ89mm. This is achieved through the precise arrangement of 7 flat and 8 vertical forming rollers, as well as 6 flat and 6 vertical sizing rollers, which can be calibrated to ensure the final diameter meets the required specifications.
The straightening machine eliminates internal stresses and physical bending that occur after the forming and welding process. By using a combination of active lower rollers and passive upper rollers pressed by a worm gear, it ensures the pipe is perfectly straight and compliant with industrial standards.
Conclusion
The implementation of high-precision welded pipe equipment is fundamental to achieving industrial-grade tubing that meets rigorous safety and quality standards. From the initial uncoiling of Q195-Q345 steel to the final stress relief in the straightening machine, every component—including the 250KW main drive and the computer-controlled flying saw—works in harmony to ensure diameter precision (φ76-φ89mm) and length accuracy (±3 mm).
As the industry moves toward greater automation and sustainability, the ability to produce thick-walled pipes (up to 5.0mm) with high efficiency (80m/min) will be a key differentiator for manufacturers. We recommend investing in equipment that balances raw power with digital control to minimize material waste and maximize output. For more information on high-performance piping solutions, visit our website: www.xhequipment.com