The global demand for high-precision industrial piping and tooling has reached an unprecedented peak as infrastructure projects evolve toward greater durability and tighter tolerances. In the realm of high-pressure fluid transport and structural integrity, the selection of materials like seamless erw pipe becomes a critical decision for engineers aiming to minimize failure rates and optimize operational longevity.
Understanding the nuances of pipe manufacturing—ranging from the forged roll mold processes to advanced thermal treatments—is essential for maintaining safety standards in heavy industry. While many focus solely on the final dimensions, the true value lies in the metallurgical integrity achieved through repeated forging and precise quenching, ensuring that components can withstand extreme mechanical stress without deformation.
By integrating rigorous quality control and precise thermal cycles, manufacturers can deliver a seamless erw pipe solution that balances hardness and toughness. This comprehensive approach not only enhances the wear resistance of the final product but also ensures that every piece meets the strict international standards required for modern machining and industrial applications.
The Industrial Significance of Seamless ERW Pipe
In the competitive landscape of metal cutting and forming machinery, the reliability of structural components is paramount. The use of high-grade seamless erw pipe ensures that systems can operate under high pressure without the risk of leakages or structural failure, which are common in lower-quality alternatives.
From an engineering perspective, the seamless nature of these components eliminates the weak points typically found in standard welded joints. This makes them indispensable for industries where safety and precision are non-negotiable, such as in the production of specialized machining molds and heavy-duty equipment.
Precision Forging and Material Preparation
The journey of a high-quality industrial component begins with meticulous material preparation. For the roll mold process, the first critical step is calculating the appropriate processing size based on the workpiece dimensions, specifically adhering to a forging ratio of 3:2-2.5 relative to the roll lower material size.
Once the dimensions are set, the raw material is subjected to an intense heating process, reaching temperatures between 850°C and 1000°C. This allows for the initial forging, where the material is shaped and repeatedly worked to achieve the designated volume and density required for a seamless erw pipe application.
This repeated forging process, typically occurring 2 to 4 times with intervening reheating cycles, is what distinguishes premium components. By refining the internal grain structure, the material becomes more compact and stable, which directly correlates to improved wear resistance during long-term industrial use.
Thermal Processing for Enhanced Durability
Thermal treatment is the heart of material science in the production of a seamless erw pipe. After the primary forging is complete, the workpiece undergoes a critical stabilization phase where it is heated to between 780°C and 830°C and held for a full 72 hours.
This prolonged heating period ensures that internal stresses are relieved and the metallurgical organization is fully homogenized. For anyone specifying a seamless erw pipe for heavy-duty machining, this step is what prevents premature cracking and ensures the tool can handle repeated impact.
Following the stabilization, the workpiece enters the quenching phase. It is placed in a quenching furnace and gradually warmed to 930-980°C before undergoing physical cooling. This rapid temperature change is essential to lock in the desired hardness, although the result is initially unstable and requires further tempering.
Mechanical Processing and Dimensional Accuracy
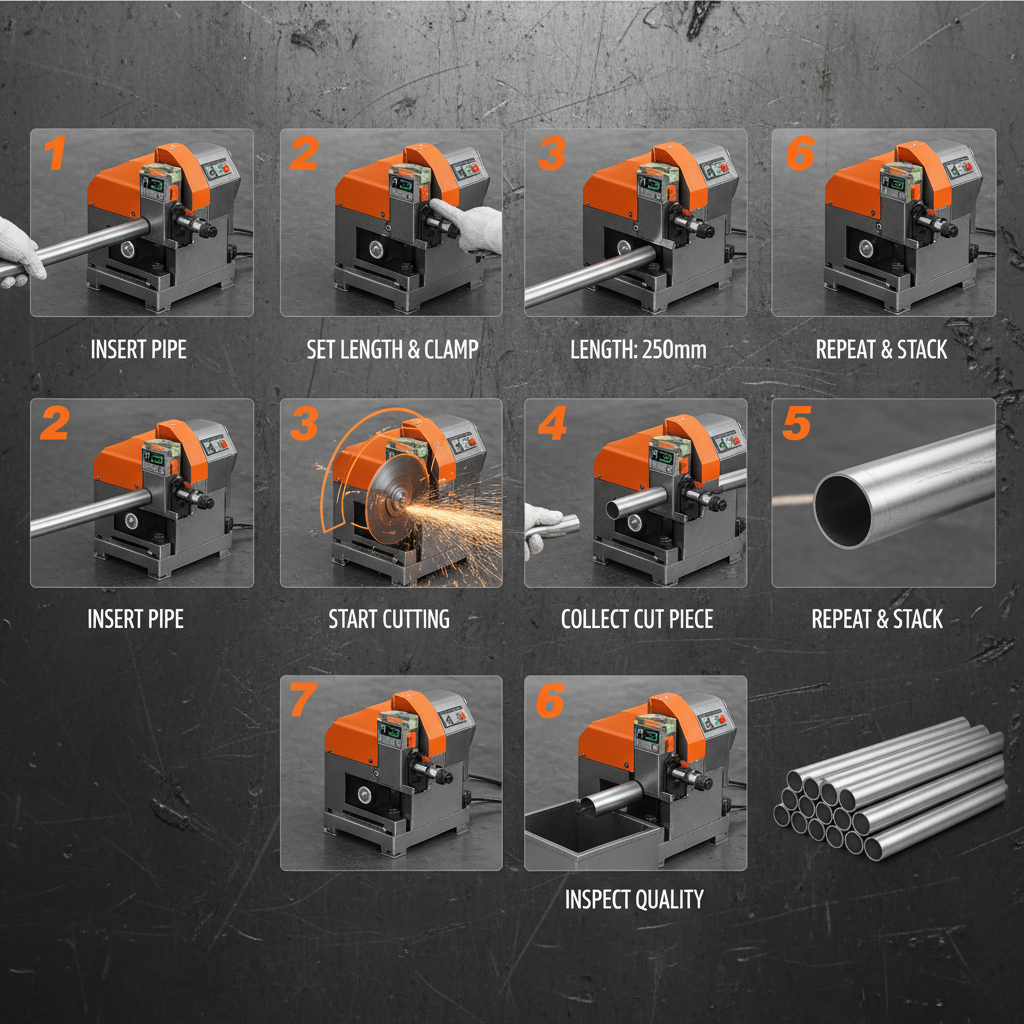
Once the thermal foundations are laid, the workpiece moves to the rough processing stage. Here, the machine focuses on creating the primary shape, cutting the inner holes, and using a hole lathe to ensure the dimensions strictly follow the technical drawings. Any designated logos or identification markers are also processed at this stage.
The precision of these cuts is vital, as the final finishing stages depend on a perfectly balanced rough shape. Whether the component is intended for a seamless erw pipe assembly or a custom mold, the adherence to the drawing's tolerances prevents misalignment in the final machine integration.
Comparative Performance of Piping Methods
Hardness Detection and Quality Assurance
The final phase of production is dedicated to verification. Low-temperature tempering is applied to stabilize the hardness achieved during quenching. Following this, a rigorous hardness detection process is implemented to ensure the workpiece falls within the strict range of 58° to 62°.
Only after the hardness is confirmed does the product enter final finishing. This includes planar finishing, inner hole polishing, and well-finishing. Every step is monitored by professional quality inspectors to ensure that the final seamless erw pipe components deliver maximum reliability to the end user.
Global Applications in Modern Machinery
High-precision forged components and seamless erw pipe are utilized across a variety of global industries. In the aerospace and automotive sectors, these materials are used in the construction of high-pressure hydraulic systems and engine components where failure is not an option.
In remote industrial zones, such as oil and gas extraction sites, the corrosion resistance and structural strength of these pipes are tested daily. The ability to withstand extreme temperature fluctuations makes these forged solutions ideal for harsh environments.
Furthermore, in the field of precision machining, these materials serve as the backbone for high-accuracy molds. The consistent hardness (58°-62°) ensures that the molds maintain their shape over thousands of cycles, reducing downtime and maintenance costs for manufacturers.
Future Trends in High-Precision Piping
The future of seamless erw pipe manufacturing is moving toward the integration of smart alloys and automated thermal monitoring. By utilizing IoT sensors during the 72-hour stabilization period, manufacturers can ensure perfect uniformity across every batch of material.
Sustainability is also becoming a core focus. New methods of "green forging" are being explored to reduce the energy consumption of the quenching and tempering furnaces without compromising the final hardness ratings of the workpiece.
As digital transformation hits the machining industry, the shift toward "Industry 4.0" will allow for the custom-tailoring of roll mold processes. This means the forging ratios and thermal cycles can be adjusted in real-time based on the specific molecular properties of the raw material batch.
Core Analysis of High-Precision Manufacturing Specifications
| Process Stage |
Key Parameter |
Quality Impact |
Standard Value |
| Initial Forging |
Forging Ratio |
Material Density |
3:2 - 2.5 |
| Primary Heating |
Temp Range |
Plasticity |
850°C - 1000°C |
| Stabilization |
Duration |
Internal Stress Relief |
72 Hours |
| Quenching |
Peak Temp |
Initial Hardness |
930°C - 980°C |
| Hardness Test |
HRC Range |
Wear Resistance |
58° - 62° |
| Final Finish |
Tolerance |
Fit & Seal |
Micron Precision |
FAQS
The final hardness for our forged components, such as those used in a seamless erw pipe application, is strictly controlled between 58° and 62°. This is achieved through a precise cycle of quenching at 930-980°C followed by low-temperature tempering, ensuring the tool possesses maximum wear resistance without becoming brittle.
The 72-hour period at 780°C to 830°C is critical for the metallurgical stabilization of the material. This prolonged thermal soak ensures that the internal organization of the metal is homogeneous and that all residual stresses from the repeated forging process are relieved, preventing warping during final machining.
A forging ratio of 3:2 to 2.5 is used to ensure that the raw material is sufficiently compressed and refined. This ratio optimizes the grain structure, making the resulting seamless erw pipe significantly more durable and resistant to mechanical fatigue compared to materials with lower forging ratios.
After hardness is verified, the finishing process includes three primary stages: planar finishing for perfectly flat surfaces, inner hole finishing for precise diameters, and overall well-finishing to remove any surface imperfections, ensuring the product is ready for immediate industrial integration.
Yes, the third step of our process involves rough machining where the shape, inner holes, and specific logos are processed in the designated positions according to the customer's technical drawings. This ensures brand traceability and specific identification for every component.
Quality is guaranteed through a multi-step inspection regime. Professional quality inspectors monitor every stage—from the initial forging ratio to the final hardness detection. Only pieces that consistently hit the 58°-62° hardness mark and pass dimensional checks are shipped to customers.
Conclusion
The production of a high-performance seamless erw pipe is a complex symphony of thermal science and mechanical precision. By strictly adhering to forging ratios of 3:2-2.5, utilizing a rigorous 72-hour stabilization period, and maintaining a precise hardness range of 58°-62°, manufacturers can provide tools that offer exceptional wear resistance and structural stability. This disciplined approach to metallurgy transforms raw steel into a critical industrial asset capable of withstanding the most demanding environments.
Looking forward, the industry must continue to embrace the balance between traditional forging expertise and modern digital monitoring. As precision requirements tighten, the commitment to "striving for fine" in every processing step will remain the only way to ensure customer satisfaction and operational safety. For those seeking the pinnacle of machining durability, investing in components forged with these exacting standards is the most reliable path to long-term success. Visit our website: www.xhequipment.com