Achieving precise dimensional tolerance and consistent weld integrity is the primary challenge in high-volume steel pipe manufacturing. When working with strip steel thicknesses between 2.0mm and 5.0mm, the transition from a flat coil to a rigid cylindrical form requires a highly synchronized sequence of leveling, forming, and sizing.
The mechanical complexity of these operations often leads to production bottlenecks, particularly during the cutting and straightening phases. For manufacturers targeting pipe diameters in the φ76-φ89mm range, the integration of automated flying saws and precision straightening machines is no longer optional but a necessity for maintaining a competitive edge in length accuracy and surface quality.
Evaluating the technical configuration of a welded pipe production line requires a deep dive into the synergy between auxiliary feeding systems and the main forming unit to ensure uninterrupted material flow.


The process begins with strip steel (typically Q195-Q345) moving from a manual uncoiler through a leveling stage. The core transformation occurs when the flat strip is incrementally bent by a series of vertical and flat rollers. In a standard high-performance setup, a configuration of 7 flat and 8 vertical forming rollers ensures that the material reaches the required φ76-φ89mm diameter without introducing excessive internal stress.
Once the circular shape is approximated, the sizing unit (using 6 flat and 6 vertical rollers) refines the final dimensions. This multi-stage reduction is critical for maintaining a wall thickness of 2.0-5.0mm, as any abrupt deformation would compromise the structural integrity of the pipe wall.
To ensure continuous production, the feeding system must eliminate tension fluctuations. A four-roller delivery machine, powered by an 18.5KW motor, manages the material flow into a cage looper. This looper acts as a buffer, decoupling the uncoiling speed from the forming speed, which prevents the strip from snapping or buckling during high-speed runs of 60-80m/min.
The structural rigidity of the machine is anchored by the materials used in the shafts. Utilizing 40Cr steel that has undergone quenching and tempering for horizontal shafts (Ф100mm) and vertical shafts (Ф60mm) prevents shaft deflection under the immense pressure of the sizing process. This metallurgy is essential for maintaining the 0-6mm length accuracy required in industrial specifications.
Furthermore, the transmission efficiency is handled by spiral bevel gearboxes made of ZG35# with a gear module of m=12. This ensures that the 250KW DC motor delivers consistent torque to the rollers, minimizing vibration that could otherwise cause "chatter" marks on the pipe surface.
The efficiency of a pipe mill is often determined by how it handles the "Turkish ear" or the pipe end closure. A specialized head with 8 rollers (4 per side) is employed to ensure the pipe remains stable as it exits the sizing unit and enters the cooling water tank.
Precision in the sizing stage (6 flat/6 vertical roller arrangement) is the primary determinant of whether a pipe will meet strict outer diameter tolerances (φ76-φ89mm) across lengths of up to 8 meters.
Following the cooling process, the pipe must be straightened. A four-column frame straightening machine using GCr15 rollers (HRC60-65) eliminates residual stresses. By maintaining a 30° angle between the straightening roller and the pipe, the machine corrects bending without distorting the circularity of the cross-section.
In the context of a welded pipe production line, there is a constant trade-off between forming speed and dimensional accuracy. While speeds of 80m/min maximize throughput, they increase the risk of length deviations during the flying saw operation.
A computer-controlled flying saw is employed to mitigate this. With a maximum sawing frequency of 15 times per minute and a precision of ±3 mm, the system synchronizes the saw car's travel with the pipe's linear speed, ensuring that the fixed length (4-8m) is maintained regardless of the production velocity.
In a typical industrial setting, such as the production of structural piping for construction, the ability to handle varying strip steel grades (Q195 to Q345) is vital. Manufacturers must adjust the pneumatic pressing platforms and hydraulic cutting systems to accommodate the different yield strengths of these materials, as stiffer steel requires higher extrusion forces in the sizing unit to avoid "spring-back."
For operations focusing on high-precision conduits, the integration of a dedicated straightening machine is the final quality gate. By eliminating the bending caused by the welding heat, the resulting pipes meet the stringent requirements for automatic coupling or high-pressure fitting, reducing the scrap rate in subsequent machining processes.
The shift toward "Smart Manufacturing" in the metal-forming sector is primarily focused on reducing labor intensity and human error. Automated shearing and welding systems are replacing manual interventions, allowing for a more consistent weld bead and reducing the downtime associated with manual coil changes.
Modern systems are now incorporating real-time speed measurement and feedback loops between the flying saw and the main motor. This allows the production line to automatically adjust the feeding speed (up to 140m/min for delivery machines) based on the current processing capacity of the sizing unit, maximizing the overall equipment effectiveness (OEE).
Future developments are likely to emphasize the use of advanced alloys for rollers to extend tool life and the implementation of AI-driven quality inspection systems that can detect weld defects in real-time without slowing down the production line.
Selecting the right machinery requires a balanced analysis of raw material specifications and desired output quality. A line designed for 2.0mm strip steel cannot be simply "overclocked" to handle 5.0mm steel without risking motor burnout or roller deformation.
The choice between a manual uncoiler and an automated feeding system depends on the volume of coil changes. For plants processing 5-ton coils frequently, the time saved by pneumatic expansion and automated delivery machines significantly impacts the daily tonnage output.
Ultimately, the synergy between the main forming unit and the auxiliary machines—such as the straightening machine and the flying saw—determines the final product's marketability.
| Selection Factor | Low-Volume Setup | Industrial Standard | High-Precision Requirement |
|---|---|---|---|
| Feeding System | Manual Uncoiler | 4-Roller Delivery | Automated Cage Looper |
| Forming Logic | Basic Bending | 7 Flat / 8 Vertical | Customized Multi-Stage |
| Cutting Method | Manual Shear | Computer Flying Saw | High-Sync Flying Saw |
| Post-Processing | Basic Cooling | Standard Straightening | Precision GCr15 Straightening |
| Material Range | Single Grade (Q195) | Q195 - Q345 | Wide Grade Compatibility |
| Accuracy Target | ±10 mm | ±3 mm (Cutting) | ±1 mm (Customized) |
Strip steel thickness (e.g., 2.0-5.0mm) directly dictates the required torque and the material of the rollers. Thicker steel increases the resistance to deformation, requiring rollers made from hardened materials like 40Cr or GCr15 to prevent premature wear. Additionally, the number of forming and sizing rollers must be sufficient to distribute the deformation stress across multiple stages, avoiding material fracture or uneven wall thickness.
The cage looper serves as a critical buffer zone between the uncoiler/delivery section and the main forming machine. It stores a specific length of raw steel strip, allowing the forming machine to run at a constant speed even if there are minor interruptions or speed variations in the feeding stage. This ensures continuous production and prevents the forming rollers from running dry, which would cause significant downtime.
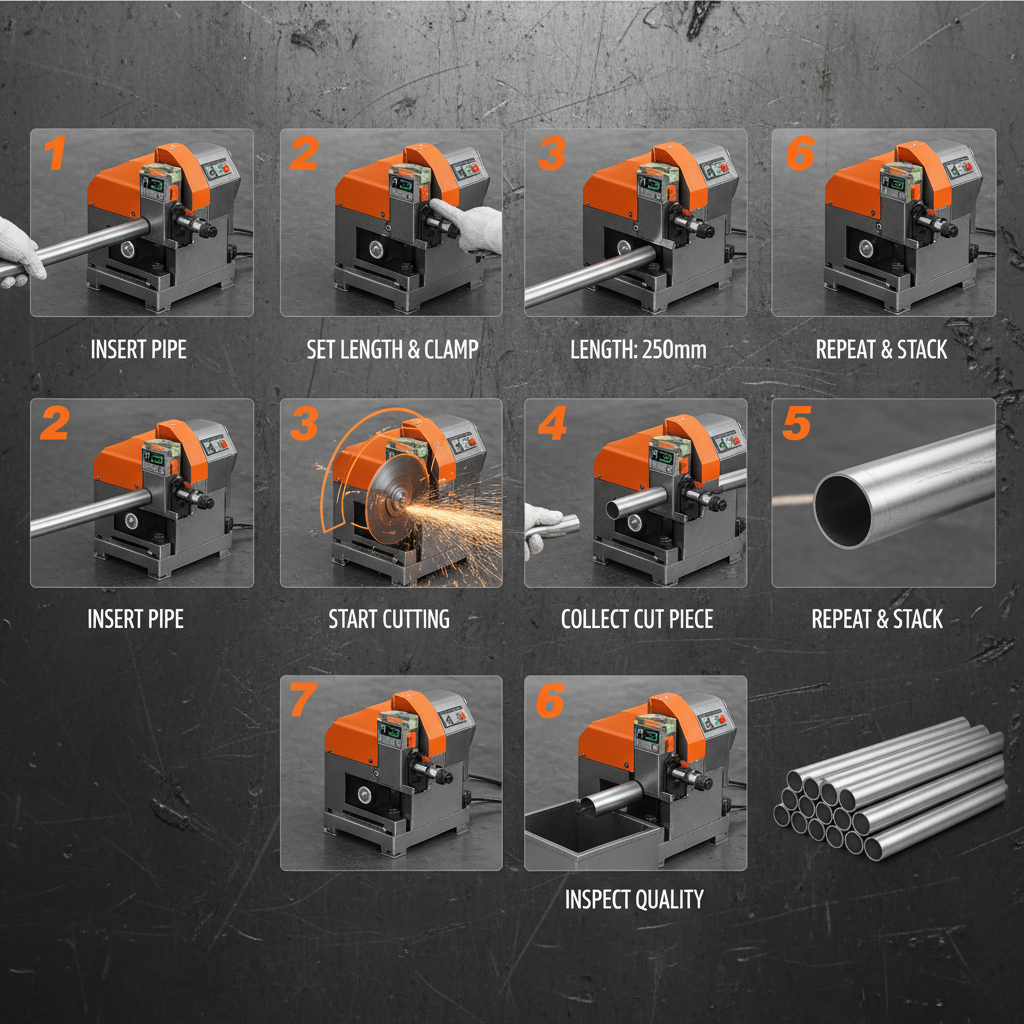
A computer-controlled flying saw allows the pipe to be cut while it is still moving at production speeds (up to 80m/min). Stationary cutting would require the entire line to stop and restart for every single pipe, which would drastically reduce throughput. The flying saw's ability to synchronize its travel speed with the pipe's speed ensures a clean, square cut and high length accuracy (±3 mm) without sacrificing velocity.
The process of welding and forming introduces internal thermal and mechanical stresses, which often cause the pipe to bow or warp as it cools. The straightening machine uses a series of precision rollers to apply calculated pressure, "pushing" the pipe back into a perfectly linear form. This is essential for pipes that will be used in structural applications where precise alignment is required for welding or assembly.
High-speed rollers, especially those made from GCr15 and quenched 40Cr, require regular lubrication and surface inspection. Because they operate under extreme pressure at speeds of 60-80m/min, any surface pitting or misalignment can lead to defects in the pipe. Regular calibration of the vertical and flat roller alignment is necessary to ensure the φ76-φ89mm diameter remains consistent throughout the production run.
While a specific line is optimized for a range (e.g., φ76-φ89mm), changing the pipe diameter typically requires replacing the roller sets (the molds). The flexibility of the line depends on the design of the gearboxes and the adjustability of the roller shafts. High-end systems are designed for quicker mold changes, allowing manufacturers to switch between different specifications with minimal downtime.
The technical viability of a welded pipe production line rests on the precision of its smallest components—from the gear module of the gearbox to the HRC hardness of the straightening rollers. By integrating a synchronized flow from uncoiling to straightening, manufacturers can achieve the high throughput and tight tolerances required by modern industrial standards.
As the industry moves toward greater automation, the focus will shift from simple mechanical forming to integrated digital control. Investing in robust materials and precise synchronization today ensures that production facilities can scale their capacity without compromising the structural integrity of the finished steel pipe.